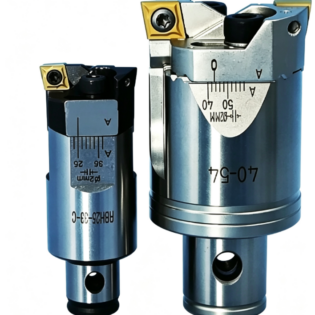
Machining relies on proper tool application to lower production costs and boost productivity. Drawing from years of on-site commissioning experience, this article starts with the principles of metal cutting. It covers tool material, cutting parameters, wiper edges, tool entering angle, machining methods and combined tools, and introduces six optimization methods to cut processing costs and raise production efficiency.
Effects of Cutting Parameters on Tool Life and Production Efficiency
To raise machining efficiency and
حياة الأداة, operators need to check whether cutting parameters are reasonable and study how each parameter affects tool life and efficiency. Cutting parameters include cutting speed, feed speed and cutting depth, known as the three key cutting factors.
Cutting Speed vc
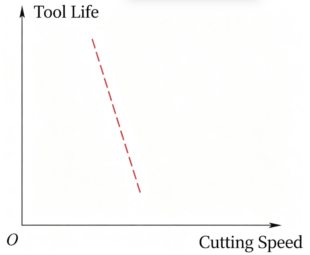
The formula linking cutting speed vc and spindle speed reads vc=πDn/1000. D stands for the effective diameter of the tool or workpiece in mm, and n means spindle speed in r/min. Excessively high cutting speed increases flank wear and worsens workpiece surface finish. Extremely high cutting speed can cause plastic deformation on cutting inserts. Figure 1 shows the curve of cutting speed versus tool life.
Figure 1 Curve of cutting speed versus tool life
Feed Speed vf
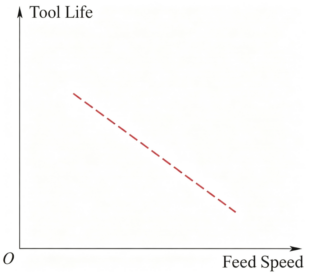
The feed speed formula is vf=fZZn. fZ refers to feed per tooth in mm/z, Zn means the number of effective cutting edges, and n is spindle speed in r/min. Too high feed speed leads to uncontrolled chips, poor workpiece surface finish and higher cutting power. Chips may strike the tool or finished workpiece surface. Figure 2 shows the curve of feed speed versus tool life.
Figure 2 Curve of feed speed versus tool life
Cutting Depth ap
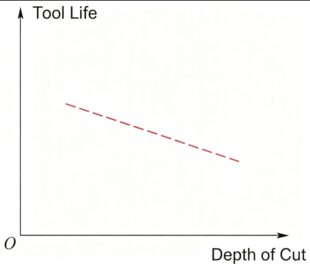
Cutting depth refers to the distance between uncut surface and finished surface. Figure 3 shows the curve of cutting depth versus tool life.
Figure 3 Curve of machining depth versus tool life
All three cutting factors affect tool life. Cutting depth has the least influence, feed speed has a larger impact, and cutting speed affects insert life most significantly.
To maximize tool life, follow these optimization rules: increase cutting depth to reduce cutting passes, raise feed speed to shorten cutting time, and lower cutting speed for longer tool service life.
For rough machining efficiency improvement, start with cutting depth adjustment. If many cutting passes exist, increase cutting depth to reduce passes. Another option is to raise cutting depth, reduce cutting speed to extend tool life, and increase feed speed to keep stable machining efficiency.
Application Case
An auto parts factory produces flanges as shown in Figure 4. The original machining plan delivers low efficiency, so workers optimize cutting parameters to extend tool life and lift productivity.
Figure 4 Flange
The team optimizes the plan by increasing cutting depth, reducing cutting passes and lowering cutting speed. The original program has messy, excessive tool paths, while optimized paths become clear, as shown in Figure 5 and Figure 6. Table 1 lists parameters before and after adjustment. After optimization, one set of tools can machine 31 parts, up from 15 parts previously.
Figure 5 Tool paths before optimization
Figure 6 Tool paths after optimization
Table 1 Parameters before and after optimization
Cutting speed defines insert cutting performance, while CNC systems read spindle speed. Many programmers only set spindle speed and ignore diameter, which greatly influences actual cutting conditions. Take turning for example: when workpiece diameter D equals 50 mm and spindle speed n equals 1000 r/min, line speed vc reaches 157 m/min. When D changes to 100 mm with the same spindle speed, vc rises to 314 m/min.
Tool catalogs show 314 m/min is an extremely high value near the limit of cemented carbide inserts. High cutting speed accelerates tool wear and shortens service life.
This example proves fixed spindle speed creates different cutting speeds with varying workpiece diameters. When tools wear quickly, check if cutting speed exceeds acceptable limits.
Effects of Wiper Edges on Cutting Efficiency
Inserts with wiper edges feature corner geometry made of 3 to 9 arcs of different radii. Arc radius can exceed 900 mm. Under identical cutting parameters, wiper edge inserts double surface finish quality. For the same surface finish requirement, wiper edge inserts allow double feed speed.
When a specific surface finish is required, wiper edge tools support higher feed speed.
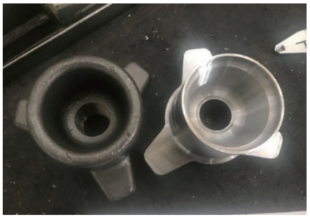
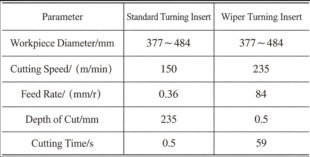
One practical case processes end faces of output housings. Workpiece material is QT500, and required surface roughness Ra ≤1.6 μm. To shorten cycle time, workers use wiper edge inserts. Feed speed rises from 0.36 mm/r to 0.5 mm/r while meeting roughness requirements. Measured Ra reaches 1.33 μm, and insert life stays unchanged. Table 2 compares parameters for standard turning inserts and wiper edge inserts. Figure 7 displays the finished output housing end face after optimization.
Table 2 Parameters for standard turning inserts and wiper edge inserts
Figure 7 Optimized output housing end face
Effects of Tool Entering Angle on Cutting Efficiency
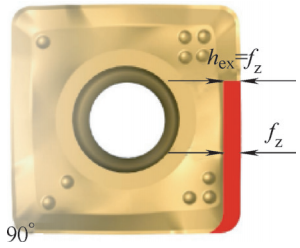
Feed per tooth connects directly to maximum chip thickness and tool entering angle. For a 90° entering angle, fz equals hex, so maximum chip thickness matches feed per tooth. Smaller entering angles allow higher feed speed.
Take square shoulder mills shown in Figure 8 for comparison. A 90° square shoulder mill has 5 cutting edges. When n equals 1000 r/min and hex equals 0.2 mm, fz equals 0.2 mm/z. Feed speed vf = 0.2 × 5 × 1000 = 1000 mm/min.
a) Structure diagram of square shoulder mill
b) Physical product
Figure 8 90° square shoulder mill
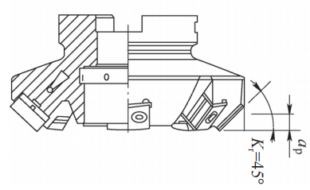
A face mill with 45° entering angle is shown in Figure 9. It also has 5 cutting edges. With n at 1000 r/min and hex at 0.2 mm, fz = hex /sin45° = 0.282 mm/z. Feed speed vf = 0.282 × 5 × 1000 = 1410 mm/min.
a) Structure diagram of face mill
b) Physical product
Figure 9 Face mill with 45° entering angle
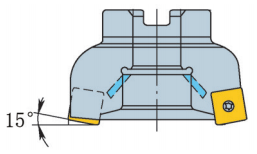
A face mill with 10° entering angle appears in Figure 10. It has 5 cutting edges. With n at 1000 r/min and hex at 0.2 mm, fz = hex /sin10° = 1.156 mm/z. Feed speed vf = 1.156 × 5 × 1000 = 5780 mm/min.
a) Schematic drawing
b) Physical product
Figure 10 Face mill with 10° entering angle
For the same inserts and spindle speed, smaller entering angles support higher feed speed. A 90° square shoulder mill mainly bears radial force with nearly zero axial force. As entering angle reduces, tools such as the 10° face mill mainly carry axial force with low radial force. Smaller entering angles increase vibration risk and power consumption.
Effects of Machining Methods on Cutting Efficiency
Tool paths strongly influence machining efficiency. Dynamic milling, a widely adopted process, uses large cutting depth and narrow cutting width for high-efficiency trochoidal cutting. Different from standard trochoidal milling, dynamic milling maintains constant chip thickness hex and delivers high metal removal rate. Constant cutting force during dynamic milling enables fast and stable machining.
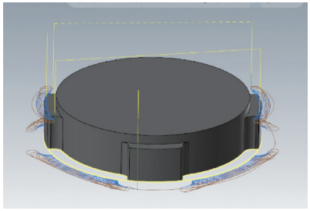
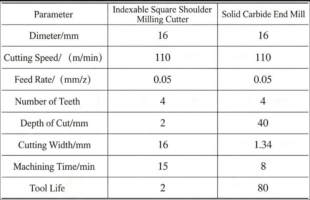
A case studies outer profile milling of valve bodies. Workpiece material is stainless steel. The tool length-diameter ratio reaches 4, which easily triggers cutting vibration. The original plan uses indexable square shoulder mills, and heavy vibration stops stable machining. The optimized plan uses solid carbide end mills with dynamic milling, large cutting depth and narrow cutting width. Figure 11 shows simulated dynamic milling paths, and Table 3 lists parameter comparison data.
Figure 11 Simulated dynamic milling paths
Table 3 Parameter comparison
Improve Cutting Efficiency with Combined Tools
Mass production often adopts combined tools to raise productivity, such as step drills and combined boring tools shown in Figure 12.
Figure 12 Combined boring tool
One combined tool completes multiple machining steps. It improves efficiency and saves tool change time for separate cutters. Combined tools carry clear drawbacks. They lack universal application, as most are custom made for specific workpieces and cannot fit other parts.
This article introduces six tool optimization methods to guide manufacturers toward higher productivity and lower production costs. Tool optimization needs flexible adjustment based on practical production. Operators first identify bottleneck processes for targeted improvement. Teams need to focus on key problems according to real workshop conditions.

 العربية
 English
 Español
 हिन्दी
 Português do Brasil
 Русский
 日本語
 Deutsch
 한국어
 Français
 Türkçe
 Polski
 Tiếng Việt
 Italiano
 简体中文